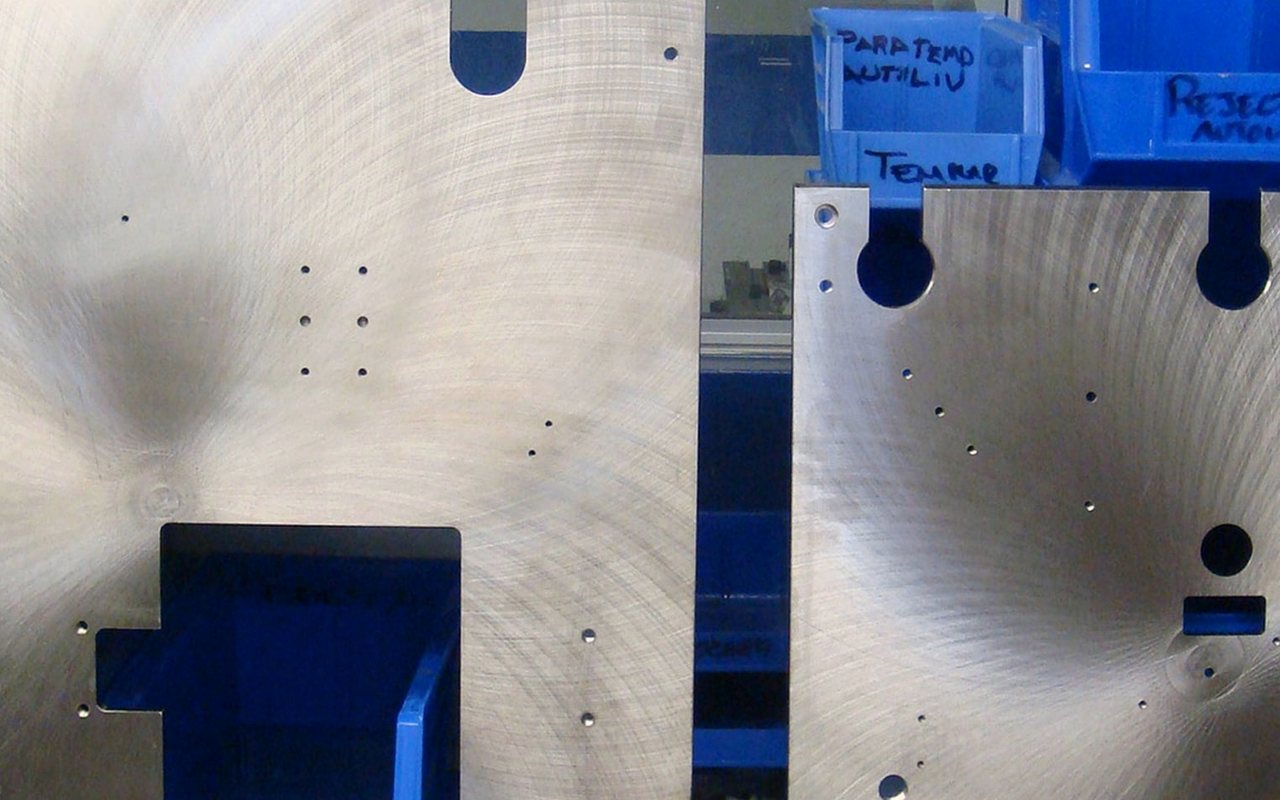
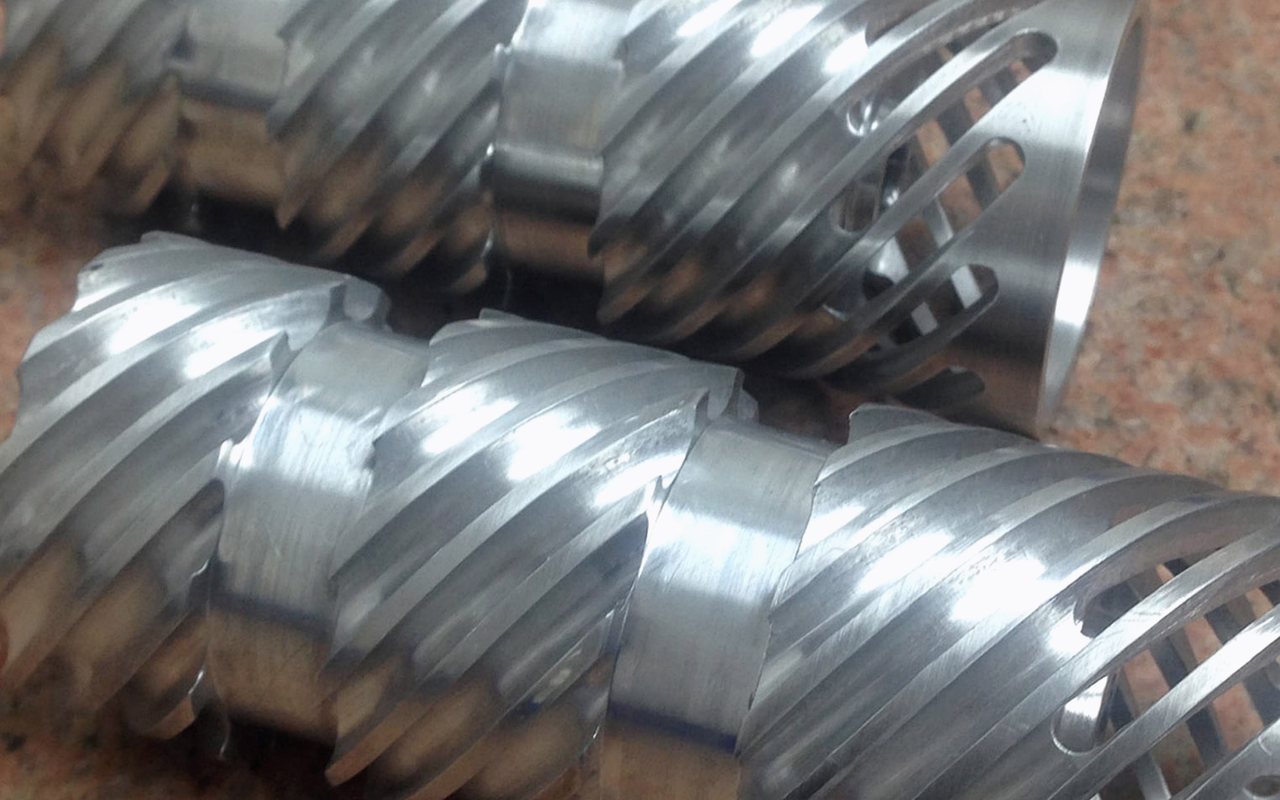
CNC Machining
Computer-controlled turning and milling for parts that have to measure exactly what the print says, from a single unit to production runs.
View this serviceWelding is easy; welding without the part moving is not. We build structures that later have to receive a machine, a robot or a precision device, so we control deposition sequence, distortion and stress relief — and when the print calls for it, we machine the mounting surfaces after welding to guarantee flatness and position.
A twisted welded base ruins the alignment of everything mounted on it. We build frames from tube and plate, control distortion with welding sequence and alternating tacks, and grind or mill the mounting faces so the machine seats on the correct plane.
We design and build transport carts, assembly tables, racks and stations sized to the available space and to operator ergonomics, with industrial casters, removable trays and a powder-coated finish.
We recover damaged structures, reinforce zones failing from fatigue and modify existing equipment for a new line or a new part number, instead of replacing the whole structure.
Distortion is not hammered out at the end: it is prevented during the process. We work on an assembly table with the piece clamped, apply alternating tacks on opposite sides instead of running a continuous bead, and control heat input so stress does not concentrate in one zone. On structures that will later receive a machine, we relieve stress before machining the mounting faces, because a plate that moves after being milled is no longer flat. That care is the difference between a base that aligns the equipment and one that forces you to shim it.
Yes. We use TIG with the right filler and shielding gas, back-purging when the application calls for it, and we passivate the heat-affected zone so the stainless keeps its corrosion resistance.
That is exactly what separates this from a general fab job. We weld, relieve stress and then machine the critical faces for real flatness and position.
Computer-controlled turning and milling for parts that have to measure exactly what the print says, from a single unit to production runs.
View this service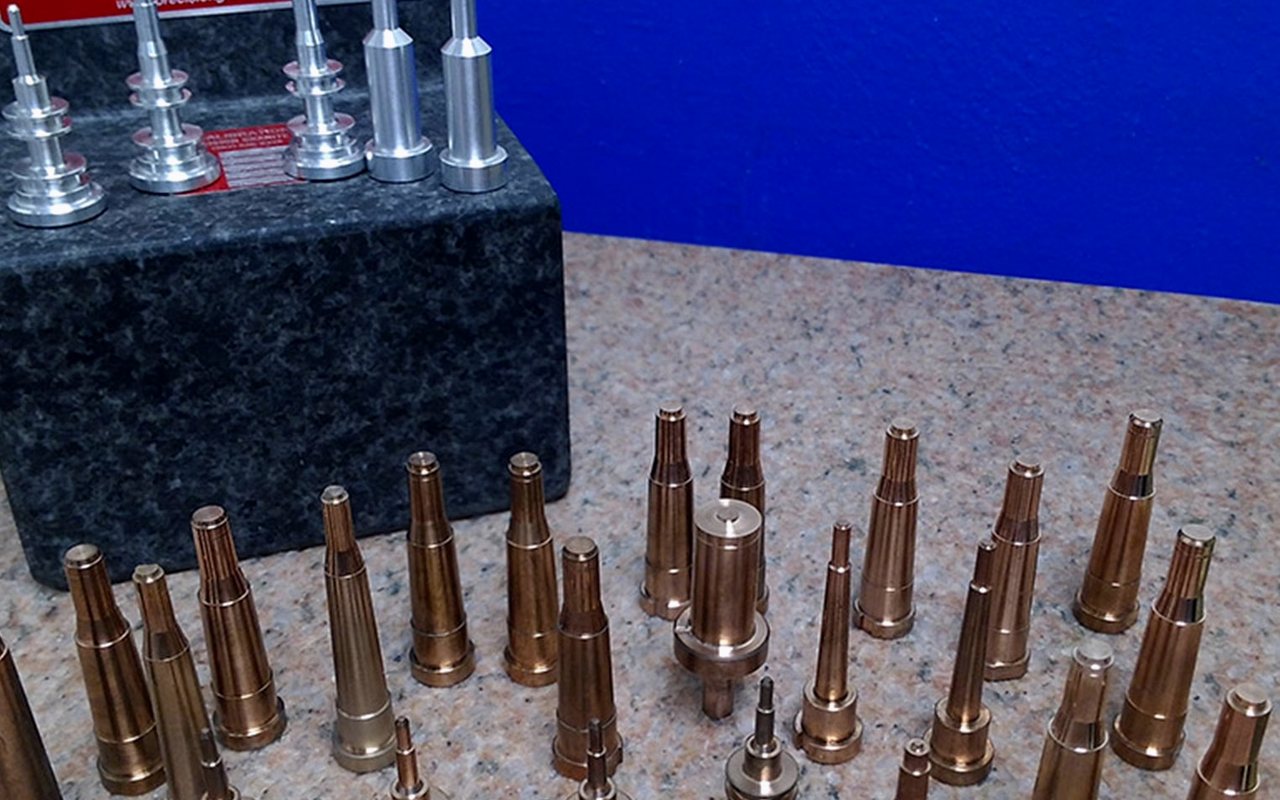
Critical parts where fit, concentricity and finish decide whether the assembly works or the line stops.
View this service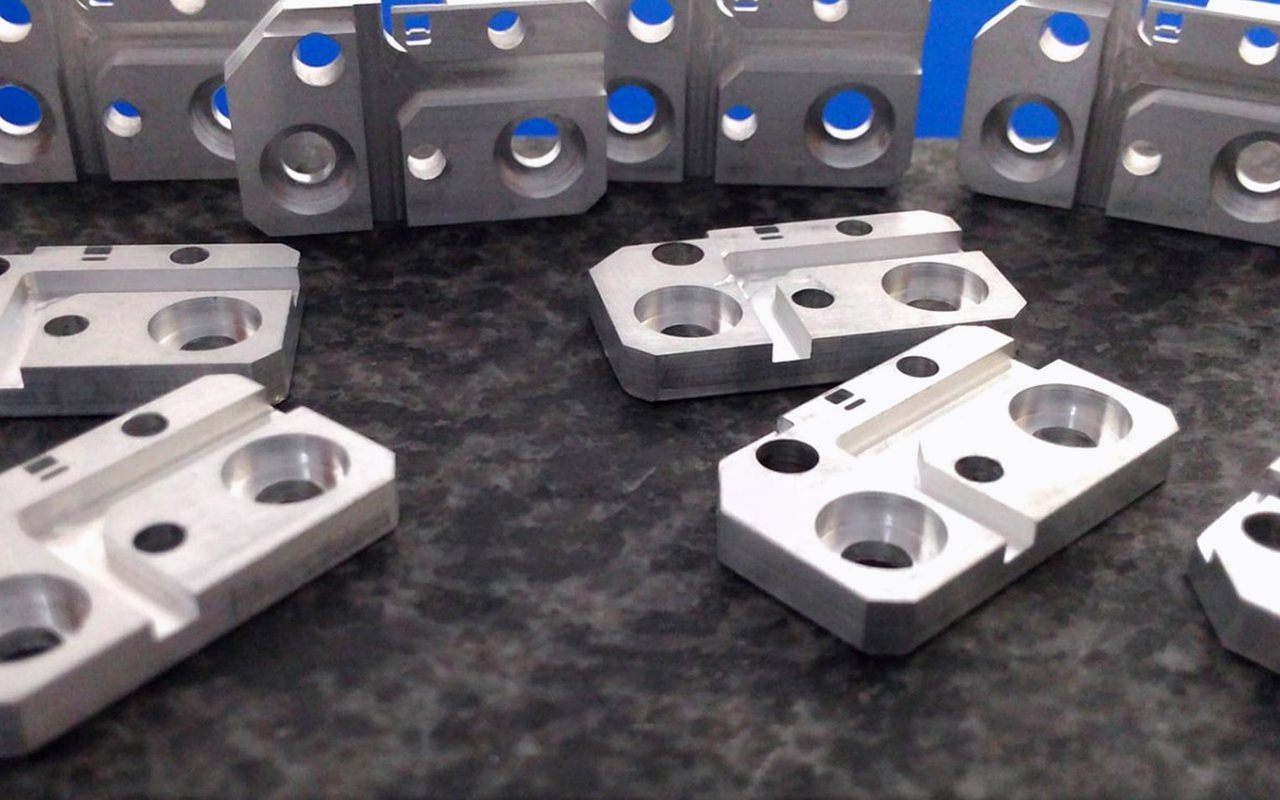
Die shoes, ground plates, punches and dies in hardened tool steel, built and maintained for real production.
View this serviceSend your drawing in PDF, STEP, IGES or DXF and get a technical and commercial proposal in under 24 business hours.